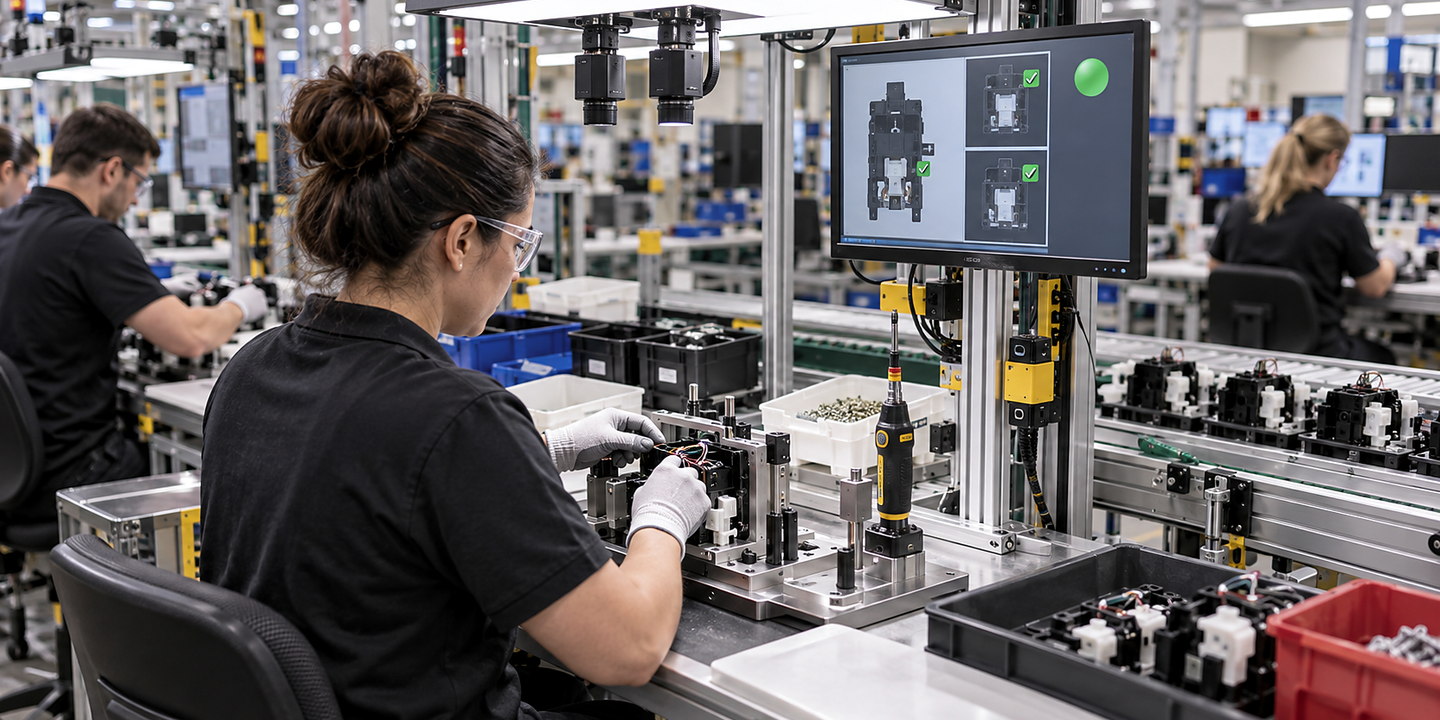
Plan mechanical, electrical, control, data, safety and operator interfaces for transparent part inspection.
In brief
Define the complete path from part presentation and inspection readiness to a result associated with the correct part or cycle. Agree who owns the settings, any reject or hold action and recovery when the expected result is unavailable. Carry these responsibilities into the acceptance-test record.
For multi-variant checks for transparent parts, define every physical connection, signal, responsibility, check and fallback before installation.
On the production floor
Connect equipment, controls and people into one reliable process — Transparent Part Inspection
Plan transparent part inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Your integration review should connect part presentation and production speed, optics, lighting and environmental conditions and the people who run the process.
Six areas to coordinate for transparent part inspection
Mechanical
Confirm how the transparent part is located and held within the required views, including the space needed for backgrounds, lighting and access. Record the normal position and orientation range and any obstruction that could hide a required region.
Electrical
For Transparent Part Inspection, list the supplies, isolation, protective devices, panels and cable routes required by the proposed installation.
Controls
Agree who initiates the inspection, confirms readiness, associates the result with the part or cycle and owns any reject or hold action. Define recipe changes, missing or late results and restart responsibilities with the line team before treating the interface as complete.
Safety
Review risk controls, stop behaviour, access, reset and the checks needed around optics, lighting and environmental conditions.
Data
Record the part or variant reference, inspection-setting revision and agreed result information needed for review. Define retention and recovery responsibilities, including how uncertain or unavailable results are distinguished from accepted results.
Your team
Plan normal operation, replenishment, clearance, cleaning, maintenance and training for multi-variant checks for transparent parts.
How the work comes together
Plan fault recovery for in-line inspection of transparent components as carefully as normal running
For Transparent Part Inspection, your team can review each stage before the complete installation is put into routine use.
01
Define the Visible Decision and Collect Representative Samples
Share representative good, bad and marginal samples, including the normal range for visible defect or measurement definition for inspection of transparent components and the difficult good, bad and marginal sample range cases.
02
Prove Contrast, Presentation and Timing in an Optical Trial
Compare suitable methods and use focused trials to show how each option performs against part presentation and production speed.
03
Integrate Cameras, Controls, Reject Handling and Recipes
Connect the equipment to your line, services and controls while resolving optics, lighting and environmental conditions for day-to-day operation.
04
Challenge Marginal Cases and Document Agreed Results
Confirm recipe, reject and line-control interfaces, then complete and record false-accept, false-reject and challenge criteria before your operating team takes over.
For your application: check part presentation and production speed, optics, lighting and environmental conditions, recipe, reject and line-control interfaces, and false-accept, false-reject and challenge criteria as part of the complete line trial.
Important limits
Line connections can change the approach for Transparent Part Inspection
A camera can only assess a property made visible and repeatable by the inspection setup.
Sample diversity and marginal cases determine how meaningful a feasibility result is.
Visual inspection does not replace hidden, destructive, functional or statutory tests.