Visible Defect or Measurement Definition for Inspection of Transparent Components: Defect and sample study
How should visible defect or measurement definition for inspection of transparent components be investigated before specifying transparent part inspection?
In brief
Start with the visible defect or measurement decision, the region to be assessed and the acceptable variation at the rejection boundary. Trial actual transparent parts with agreed backgrounds, lighting, views and presentation; record which conditions can be distinguished repeatably. Build the good, bad and marginal sample set around that decision.
For in-line inspection of transparent components, describe the realistic range and how changes in visible defect or measurement definition for inspection of transparent components affect the result you need.
On the production floor
Turn your production information into clearer decisions — Transparent Part Inspection
Plan transparent part inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Use this guide to resolve visible defect or measurement definition for inspection of transparent components before it limits the final system.
Visible Defect or Measurement Definition for Inspection of Transparent Components: condition, range and effect on your process
Current condition
Separate the agreed defect definition from its appearance in one image. Compare labelled good, bad and marginal parts under the same recorded viewing conditions, and identify the region being judged. An apparent mark needs the quality owner's classification; an uncertain or unobservable condition must not be recorded as a confirmed pass.
Realistic range
Include normal changes in part geometry and appearance as well as samples near the acceptance boundary. Record supplier, batch, age, environment and upstream process state where they affect the visible decision. A feature visible in one view is not evidence that every required surface is covered.
Effect on the system
For each decision, record the part reference, inspected region, expected result and viewing conditions used in the trial. State which changes require another optical check and which conditions remain unresolved, so the accepted definition does not silently expand to untested parts or views.
Before you contact us
Five questions about visible defect or measurement definition for inspection of transparent components for your application
Who can confirm this information?Identify the person responsible for visible defect or measurement definition for inspection of transparent components in production, quality, engineering or operations.
How representative is the sample?Include age, supplier, batch, environment and upstream process state where they affect transparent part inspection.
What is the difficult condition?Include the marginal defect and the acceptable part most easily confused with it. Record changes in background, illumination, orientation or normal appearance that make that distinction difficult, without assuming the image alone establishes the cause.
How will you judge the result?Agree the method, repetitions, acceptable range, result record and the response if the observed result falls outside the agreed range.
What else must be coordinated?Your final transparent part inspection scope must also account for recipe, reject and line-control interfaces, false-accept, false-reject and challenge criteria, current regulations and the conditions at your site.
Connected details
Review visible defect or measurement definition for inspection of transparent components as part of the complete system
Question 1
Visible Defect or Measurement Definition for Inspection of Transparent Components
For Visible Defect or Measurement Definition for Inspection of Transparent Components: Defect and sample study, describe the current position, required outcome, acceptable limits and known exceptions for visible defect or measurement definition for inspection of transparent components. That lets us compare options against your real production rather than one nominal value.
Question 2
Good, Bad and Marginal Sample Range
For Visible Defect or Measurement Definition for Inspection of Transparent Components: Defect and sample study, describe the current position, required outcome, acceptable limits and known exceptions for good, bad and marginal sample range. That lets us compare options against your real production rather than one nominal value.
Question 3
Part Presentation and Production Speed
For Visible Defect or Measurement Definition for Inspection of Transparent Components: Defect and sample study, describe the current position, required outcome, acceptable limits and known exceptions for part presentation and production speed. That lets us compare options against your real production rather than one nominal value.
Question 4
Optics, Lighting and Environmental Conditions
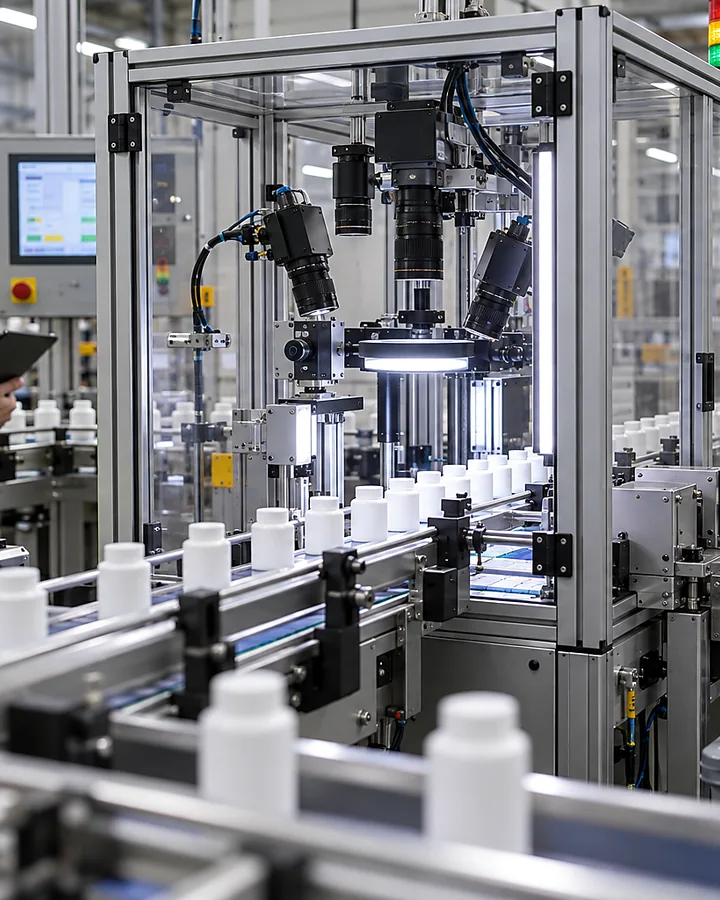
Trial the proposed backgrounds, illumination and view angles with the labelled sample set. Keep the conditions recorded with the results, including any required region that is obscured or cannot be judged consistently. Do not treat a clear image of one region as proof of complete coverage.
Question 5
Recipe, Reject and Line-Control Interfaces
For Visible Defect or Measurement Definition for Inspection of Transparent Components: Defect and sample study, describe the current position, required outcome, acceptable limits and known exceptions for recipe, reject and line-control interfaces. That lets us compare options against your real production rather than one nominal value.
Question 6
False-Accept, False-Reject and Challenge Criteria
For Visible Defect or Measurement Definition for Inspection of Transparent Components: Defect and sample study, describe the current position, required outcome, acceptable limits and known exceptions for false-accept, false-reject and challenge criteria. That lets us compare options against your real production rather than one nominal value.