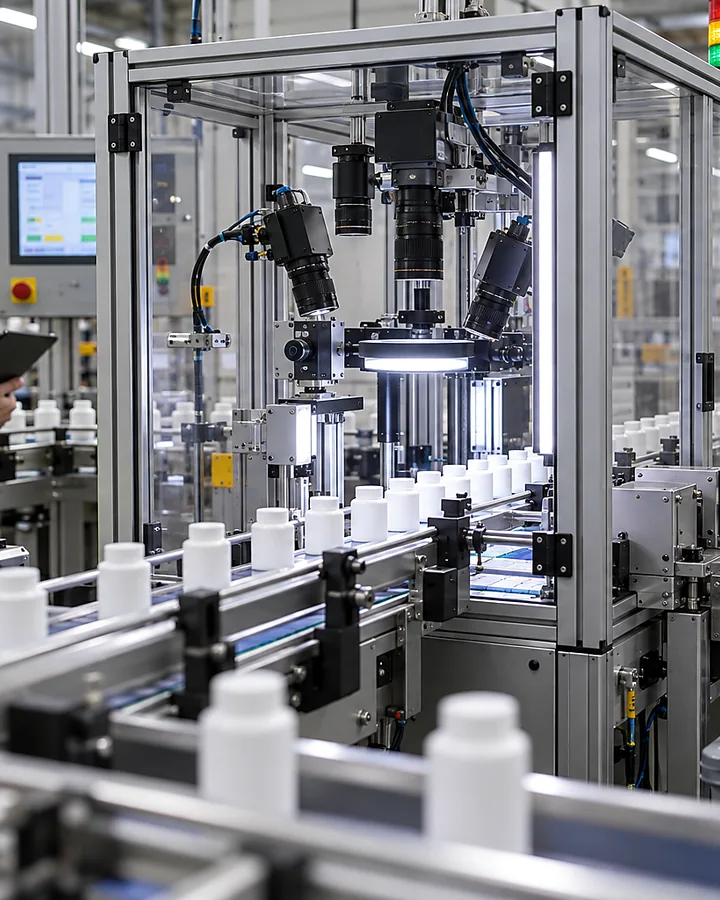
A person handling an assembly at a workstation beneath cameras and lighting.
Industrial machine vision

Transparent Part Inspection

Plan transparent part inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems.

Speak directly with Oxford Vision Systems about inspection of transparent components.

Quick answer

How can we make defects visible when inspecting transparent parts?

Supply transparent parts with acceptable variation and defects at the rejection boundary. Include scratches, contamination or shape concerns only where they form part of the required scope. Trial the background, lighting and viewing angles with realistic presentation, then document which defects and surfaces the setup can distinguish.

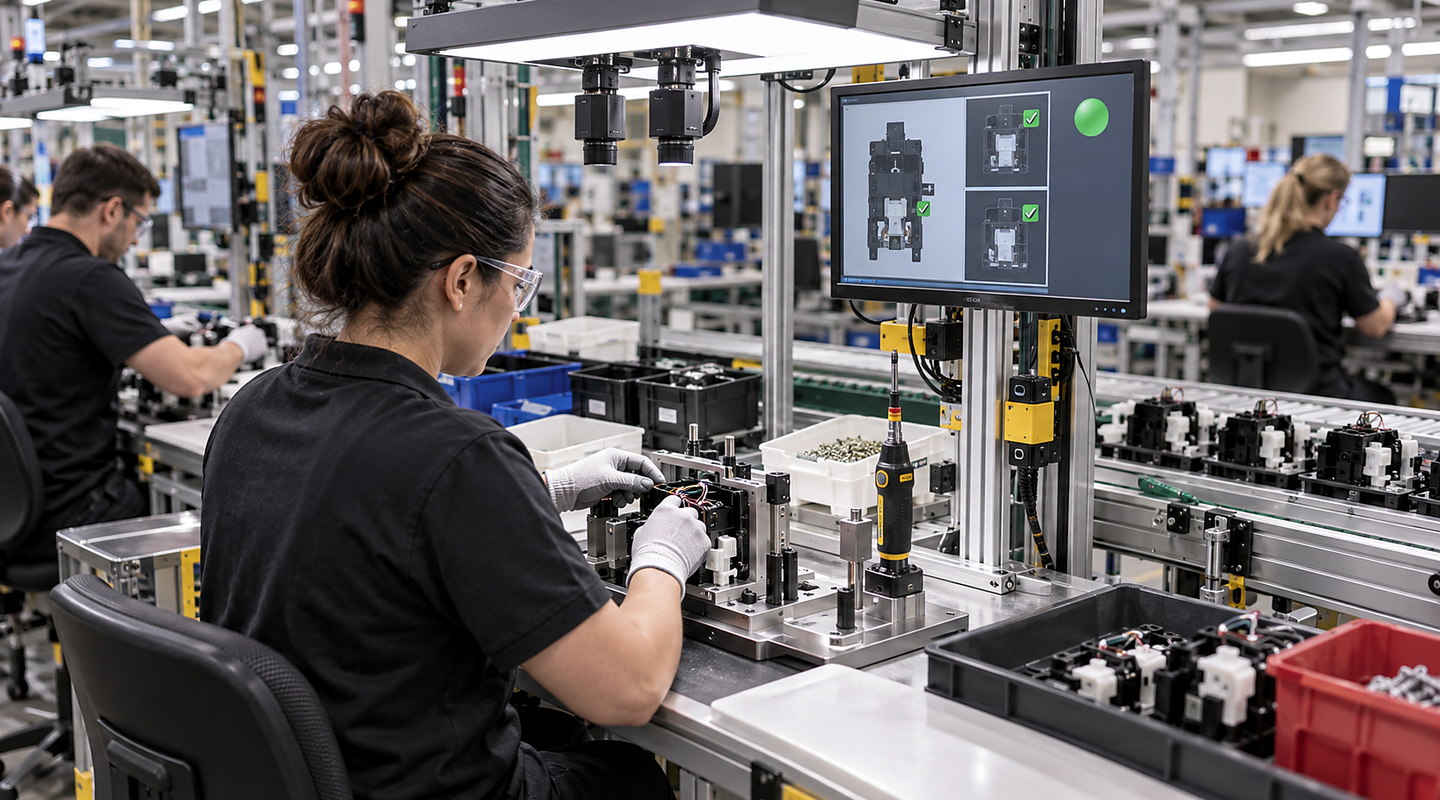
A person handling an assembly at a workstation beneath cameras and lighting.
A person adjusting camera and lighting hardware beside a conveyor.
Six useful questions

Describe what you need from transparent part inspection before choosing a solution

For in-line inspection of transparent components, share the normal condition, realistic range and difficult cases the finished system must handle.

Question 1

Visible Defect or Measurement Definition for Inspection of Transparent Components

Define the visible defect or measurement decision and its acceptable limits. Include scratches, contamination or shape concerns only where they are in scope, and identify the surfaces the optical trial must distinguish.

Question 2

Good, Bad and Marginal Sample Range

Supply representative good, bad and marginal transparent parts, including defects at the rejection boundary. Record normal variation and relevant supplier, batch, age, environment or upstream-process differences so the trial reflects the production range.

Question 3

Part Presentation and Production Speed

Describe how parts are presented and the normal and credible extremes of production speed. Trial contrast, presentation and timing under realistic line conditions, including the difficult cases the finished system must handle.

Question 4

Optics, Lighting and Environmental Conditions

Compare backgrounds, lighting and viewing angles with representative parts in the expected environment. Document which defects and surfaces the setup can distinguish, and the conditions needed to make that visible result repeatable.

Question 5

Recipe, Reject and Line-Control Interfaces

Agree operating modes, line handshakes, recipes, reject handling, faults and recovery with the line team. Define the identifiers, results and retention records needed for the agreed inspection checks.

Question 6

False-Accept, False-Reject and Challenge Criteria

Agree the false-accept, false-reject and challenge criteria, trial method, repetitions and result record. Include normal, difficult and fault conditions, and define the response when a result falls outside the agreed range.
Applications

Two useful starting points for transparent part inspection

The right choice changes with visible defect or measurement definition for inspection of transparent components, good, bad and marginal sample range, your line layout and required results.

What happens next

Your route from an initial enquiry to a working solution

You can review decisions about recipe, reject and line-control interfaces and false-accept, false-reject and challenge criteria at each stage.

  1. 01

    Define the Visible Decision and Collect Representative Samples

    Share representative good, bad and marginal samples, including the normal range for visible defect or measurement definition for inspection of transparent components and the difficult good, bad and marginal sample range cases.

  2. 02

    Prove Contrast, Presentation and Timing in an Optical Trial

    Compare suitable methods and use focused trials to show how each option performs against part presentation and production speed.

  3. 03

    Integrate Cameras, Controls, Reject Handling and Recipes

    Connect the equipment to your line, services and controls while resolving optics, lighting and environmental conditions for day-to-day operation.

  4. 04

    Challenge Marginal Cases and Document Agreed Results

    Confirm recipe, reject and line-control interfaces, then complete and record false-accept, false-reject and challenge criteria before your operating team takes over.

Important limits

Know what needs a separate check

Your final solution for inspection of transparent components must reflect the law, current standards and site-specific risks that apply to your installation.