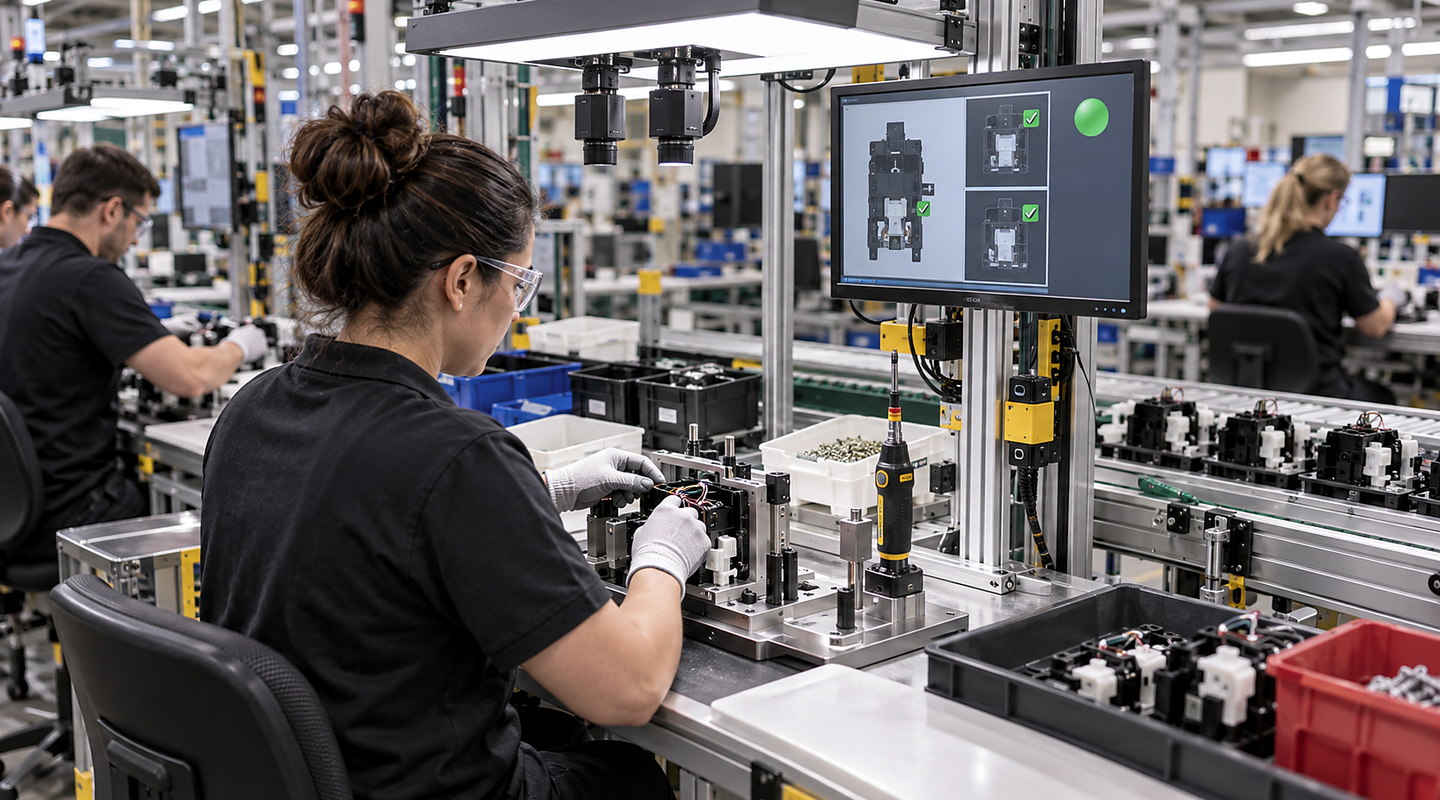
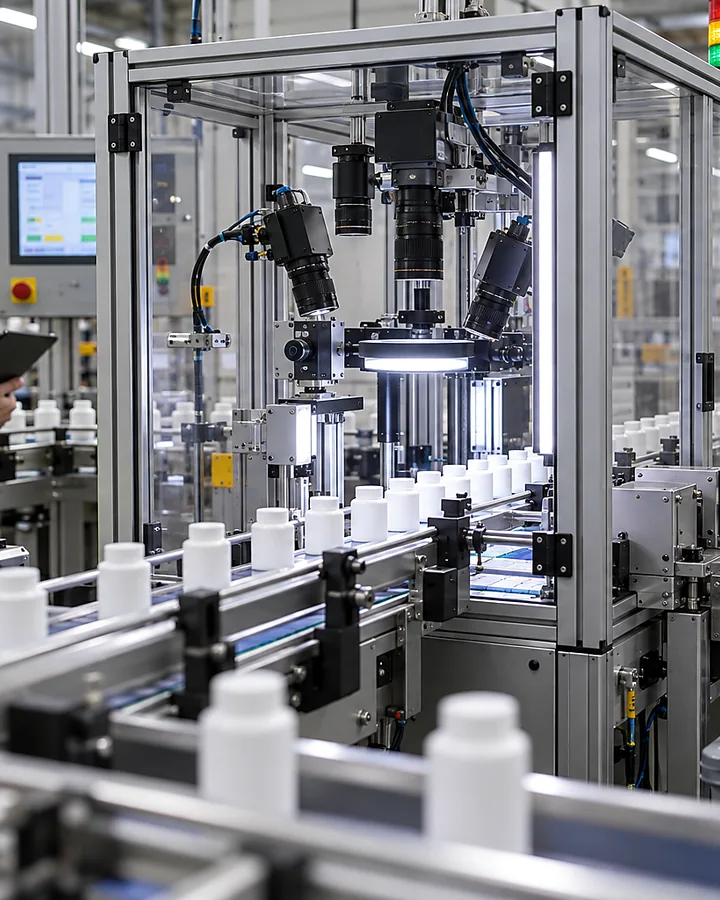
Plan in-line inspection of transparent components around representative good, bad and marginal samples under real line presentation, line connections, operating limits, acceptance checks and next steps.
In brief
An in-line trial should connect the presented transparent part, the agreed image opportunity and the result returned to the line. Test the visible decisions with realistic position, orientation and production timing, then document the response when an inspection or result is unavailable. Define responsibilities in the line-integration guide.
Plan transparent part inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems.
On the production floor
Plan for the conditions your team handles every day — Transparent Part Inspection
Plan transparent part inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. For in-line inspection of transparent components, the deciding details include visible defect or measurement definition for inspection of transparent components, part presentation and production speed and false-accept, false-reject and challenge criteria.
Details worth resolving early for in-line inspection of transparent components
Question 1
Visible Defect or Measurement Definition for Inspection of Transparent Components
State the visible decisions and regions required before the part leaves the inspection position. Keep the agreed acceptance boundaries with the trial samples, and identify any condition that cannot be assessed by the proposed views.
Question 2
Good, Bad and Marginal Sample Range
For in-line inspection of transparent components, describe the current position, required outcome, acceptable limits and known exceptions for good, bad and marginal sample range. That lets us compare options against your real production rather than one nominal value.
Question 3
Part Presentation and Production Speed
Record normal and credible presentation and speed ranges, including the positions and views needed for the agreed decision. Keep the part or cycle association through the trial so each result can be checked against the item that produced it, rather than judged from isolated successful images.
Question 4
Optics, Lighting and Environmental Conditions
Use the intended line surroundings when checking backgrounds, illumination and view angles. Record the viewing conditions with the trial results and identify changes that make the required region obscured or the decision uncertain; do not infer coverage from a stationary example alone.
Question 5
Recipe, Reject and Line-Control Interfaces
For in-line inspection of transparent components, describe the current position, required outcome, acceptable limits and known exceptions for recipe, reject and line-control interfaces. That lets us compare options against your real production rather than one nominal value.
Question 6
False-Accept, False-Reject and Challenge Criteria
For in-line inspection of transparent components, describe the current position, required outcome, acceptable limits and known exceptions for false-accept, false-reject and challenge criteria. That lets us compare options against your real production rather than one nominal value.
Your operating cycle
Plan for more than automatic running
Include replenishment, normal production, planned change, short stops, fault recovery, cleaning and maintenance for in-line inspection of transparent components. A fast automatic step can still leave your team with a slow or awkward overall process.
Normal production and variant changes
Replenishment and material presentation
Operator access and safe interventions
Cleaning, maintenance and recovery
Prove the result
Test in-line inspection of transparent components against representative good, bad and marginal samples
Normal production
Run the agreed product or part mix for in-line inspection of transparent components at your intended operating pattern.
Difficult conditions
Include credible extremes for visible defect or measurement definition for inspection of transparent components and good, bad and marginal sample range.
Fault and recovery
Agree how the line will handle a missing or late result, an interrupted cycle and an uncertain inspection outcome. Record the responsibility and expected response for each case, then include the agreed recovery sequence in the acceptance plan.
Important limits
Be clear about what the trial has shown
A camera can only assess a property made visible and repeatable by the inspection setup.
Sample diversity and marginal cases determine how meaningful a feasibility result is.
Visual inspection does not replace hidden, destructive, functional or statutory tests.